Accuromm Central Europe

A tool engineering company that supports all work related to tools

Made by ACE in Poland

One-shot processing

Carbide drill series for one-shot machining with IT7 grade hole diameter accuracy!

Astonishing finishing accuracy produced by “drilling edge” + “special reaming edge”!

IT7 grade hole diameter accuracy in one-shot

Line-up for solid holes, cast holes, and high feeds

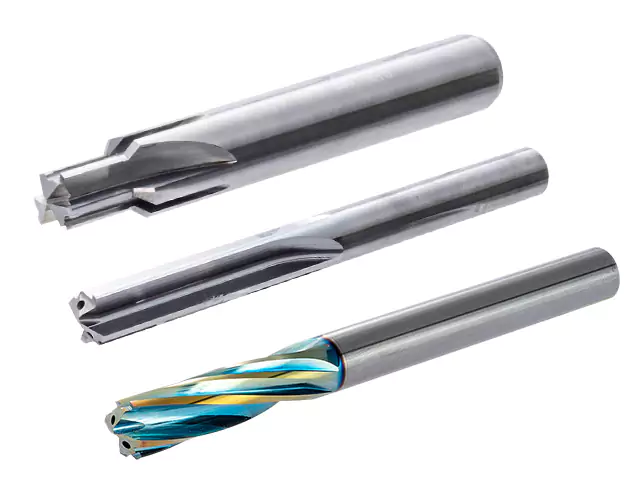
G7 drill series

What is the G7 drill series?

① G7X drill

For solid hole drilling

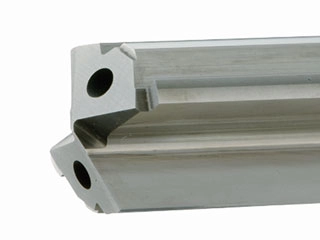
Features: High-precision machining with special reamer edges

  • Drilling edges: 2
  • Reaming edges: 2 
  • Accuracy: hole diameter IT7 grade
  • Surface roughness: 6.3z or less
  • Cylindricity: 8µm or less

② G7T drill

For cast holes drilling

Features: Stable machining even with cast holes

  • Drilling edges: 3
  • Reaming edges: 3
  • Accuracy: hole diameter IT7 grade
  • Surface roughness: 6.3z or less
  • Cylindricity: 8µm or less

PAT. PENDING

③ Y7 drill

For high feed processing

Features: High feed version of G7X with twisted flute

  • Drilling edges: 2
  • Reaming edges: 4
  • Accuracy: hole diameter IT7 grade
  • Surface roughness: 6.3z or less
  • Cylindricity: 8µm or less

Japan's Tooling Assocation ECO AWARD

Amazing facts!

── Introducing ideas and technologies ──

The G7 drill series consists of a drilling edge and a special reaming edge.
By separating each flute, chips from the cutting edge are discharged separately to eliminate chip entrapment, while the reaming edge uses a special cutting edge profile to realise one-shot drilling in IT7-grade holes.
The line-up includes the G7X drill for solid holes, the G7T drill for cast holes and the Y7 drill as a high feed version of the G7X drill.

G7X drill (solid hole)
IT7 grade hole accuracy

Good!

Hole diameter variation

G7T drill (cast hole)
IT7 grade hole accuracy

Good!

Hole diameter variation

Y7 drill (high feed)
High precision machining

Good!

Roundness vs. feed rate

This is the point!

The role of the cutting edge is divided by function

Excellent!
Optimizied phasing of drill and special reamer cutting edges prevents chips from being caught
High precision machining with special reamer cutting edges

Development / product concept

“Current status and challenges”

  • With the shift from specialised machines to general-purpose machines, the need for drill reamers that combine drill and reamer in one machine has increased in order to reduce cycle time
  • However, problems remained, such as problems caused by chip entrapment and inconsistent machining accuracy

“Development points”

  • Optimised phasing of the drill and reamer edge improves chip evacuation.
  • The reamer edge uses a special cutting edge profile to improve machining accuracy and achieves IT7-grade hole diameter accuracy.

Machining example

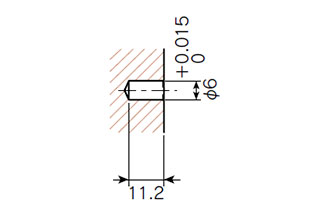
Solid hole drilling

ToolG7X drill
WorkpieceAluminium block
Work materialADC12 / ENAC-AlS11Cu2(Fe)
Tool diameterø6 mm
Cutting conditionsCutting speed: Vc = 150 m/min
Feed: f = 0.2 mm/rev
Required accuracy

Hole diameter

Surface roughness

Machining example

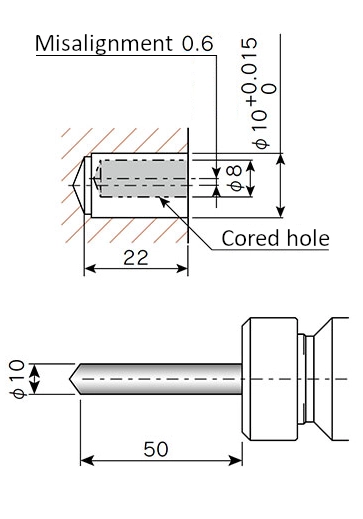
Casted hole drilling

ToolG7T drill
WorkpieceAluminium block
Work materialADC12 / ENAC-AlS11Cu2(Fe)
Tool diameterø10 mm
Cutting conditionsCutting speed: Vc = 150 m/min
Feed: f = 0.2 mm/rev
Required accuracy

Hole diameter

Roundness

Position tolerance

Product specification

ToolG7X drill
Target process

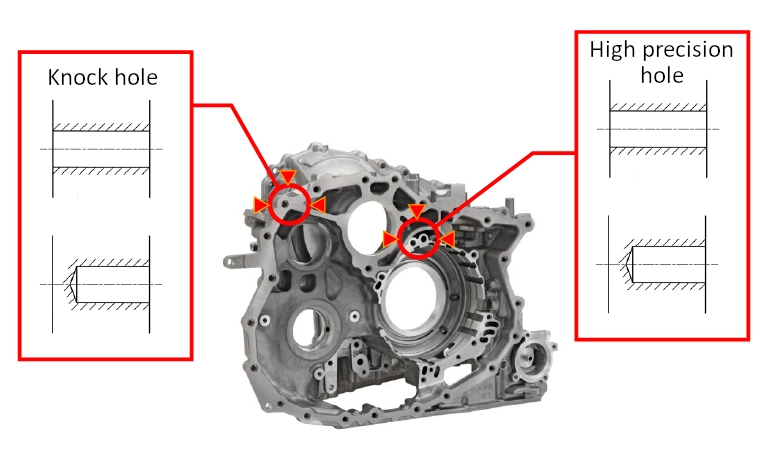
Knock hole,
Aluminium high precision hole / solid hole

*One-shot processing of solid materials

Diameter rangeø5 mm ~
Standard cutting conditions

Cutting speed: Vc = 50~200 m/min
Feed: f = 0.1~0.2 mm/rev

Machining accuracy

Hole diameter IT7 grade

ToolG7T drill
Target process

Knock hole, 
Aluminium high precision hole / cast hole

*One-shot processing of solid material

Diameter rangeø5 mm ~
Standard cutting conditions

Cutting speed: Vc = 50~200 m/min
Feed: f = 0.1~0.2 mm/rev

Machining accuracy

Hole diameter IT7 grade

ToolY7 drill
Target process

Knock hole,
Aluminium high precision hole / solid hole

*One-shot processing of solid materials

Diameter rangeø6 mm ~
Standard cutting conditions

Cutting speed: Vc = 50~150 m/min
Feed: f = 0.2~0.4 mm/rev

Machining accuracy

Hole diameter IT7 grade

Transmission case